Boron Carbide Vendor Essentials for High-Performance Material Sourcing
2026-09-20
Sourcing boron carbide for high-performance applications is rarely a straightforward task. The finest powders and sintered parts demand more than a competitive quote—they require a vendor who understands purity thresholds, particle morphology, and the unforgiving environments where your materials will perform. Whether you're engineering ballistic armor, abrasive nozzles, or neutron absorbers, the wrong supplier choice can quietly undermine your final product. Before you commit to a source, it pays to look beyond the spec sheet. What quality controls are in place? How consistent is the batch-to-batch chemistry? Does the vendor offer technical guidance when sintering behavior shifts? These questions separate transactional sellers from true material partners. In this guide, we’ll break down the vendor essentials that matter most—and show why HUAYI TECH has become a name worth knowing in advanced boron carbide supply.
What a Boron Carbide Vendor Won't Tell You About Their Powder
The particle size number on a spec sheet rarely tells the whole story. Vendors like to quote a single average diameter, but what they won't mention is how broad or skewed the distribution really is. A powder with a D50 of 1 micron could still carry a tail of 10-micron agglomerates that wreak havoc during sintering, leaving porosity and uneven grain growth. You only find out after your pressed parts come out with density gradients and microcracks that trace back to those hidden coarse fractions.
Oxygen and free carbon are the quiet killers in boron carbide, and most suppliers would rather not discuss them. A thin oxide layer on the particle surfaces raises the sintering temperature and reduces the final hardness, while even small variations in free carbon shift the boron-to-carbon ratio away from the stoichiometric sweet spot. The certificate might list total oxygen and total carbon, but it won't separate surface-bound oxygen from bulk impurities, nor tell you whether that carbon is present as graphite, carbide, or organic residue. Each form behaves differently in the furnace.
Batch-to-batch consistency is another uncomfortable topic. Powder sourced from different ore deposits or blended with recycled material can change the impurity profile and sinterability without any notice. A vendor won't volunteer that the incoming raw material shifted or that a milling parameter was tweaked, yet your pressing pressure and firing schedule suddenly need re-optimization. Worse, some lots may contain trace metals like iron or silicon from the grinding media, which act as unintended sintering aids or form brittle secondary phases. By the time you run a full analysis, the lot is already in your production line.
Checking for Consistency Before You Place a Large Order
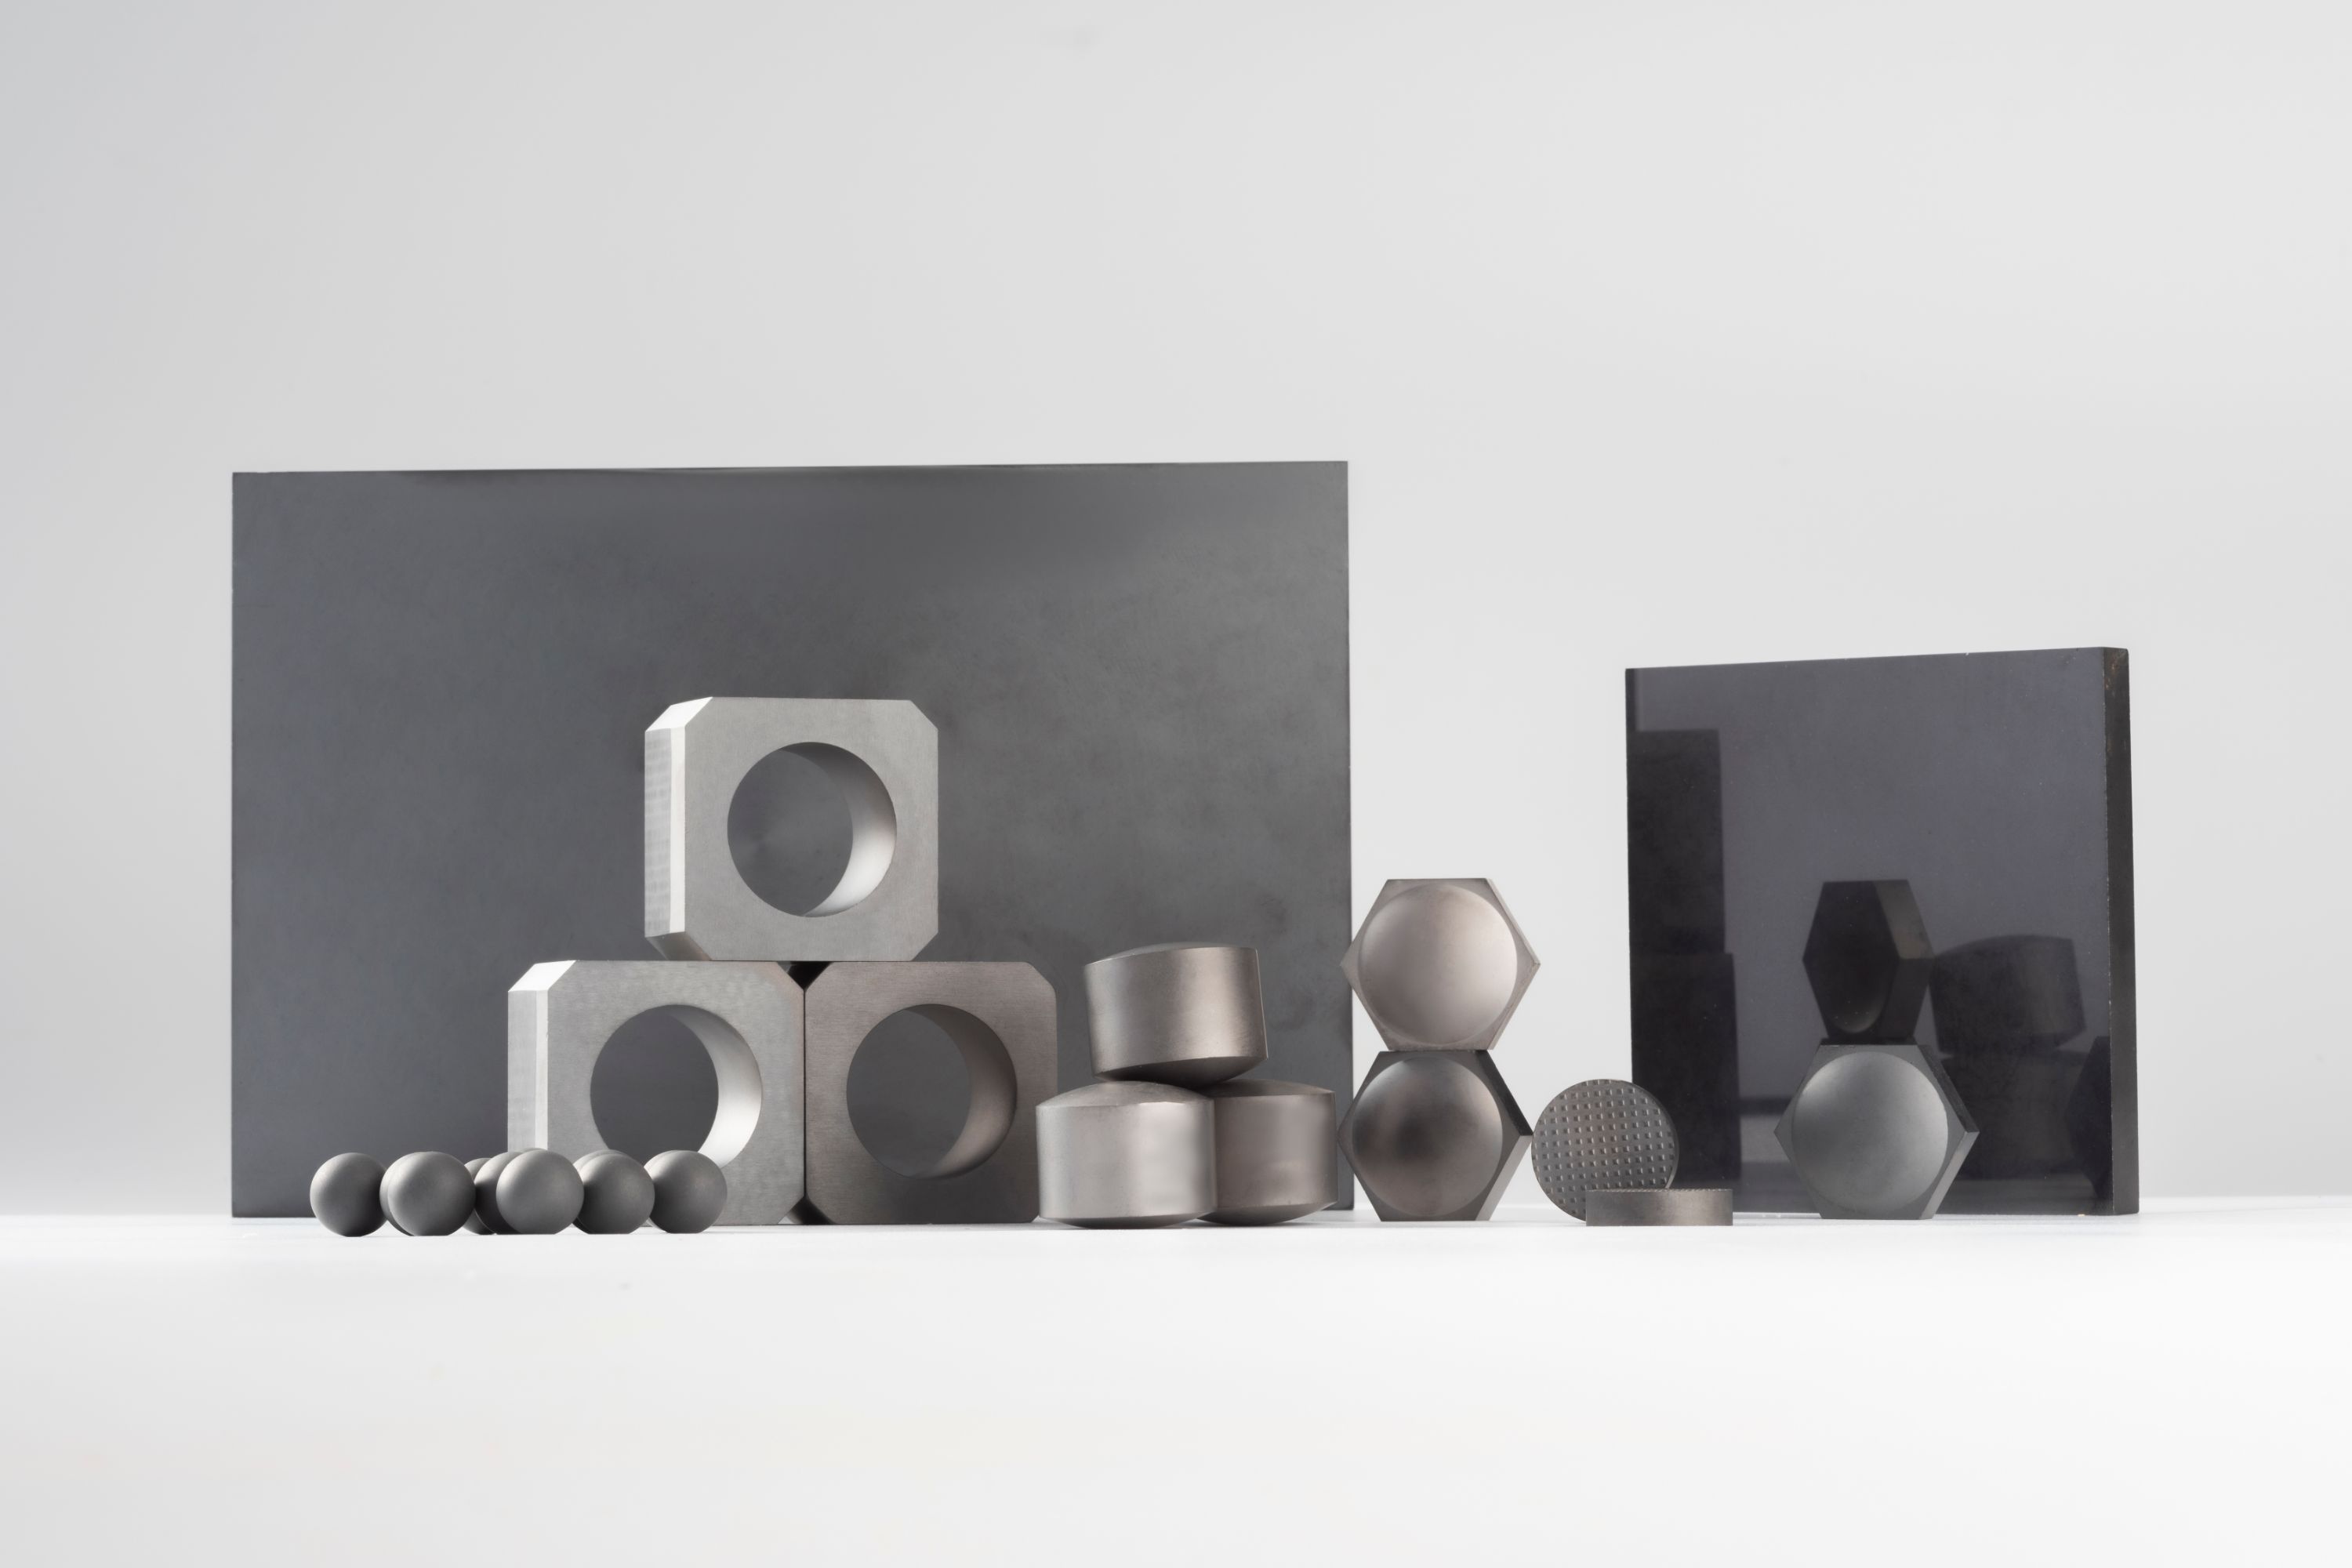
A single sample can be misleading. Colors shift between dye lots, fabric weights drift from one production run to the next, and even the thread tension on a stitching line can vary when machines are recalibrated. Before committing to hundreds or thousands of units, ask your supplier to pull samples from at least two separate batches, not just the master sample they keep on the shelf. Compare them side by side under the same lighting you would use for final inspection, and measure anything that matters: color, thickness, dimensions, logo placement, and packing method.
It is also worth asking for a documented tolerance range for each critical spec. If the supplier cannot tell you how much variance to expect, that is a red flag. A tolerance of plus or minus two millimeters might be fine for the outer carton, but it could ruin a die-cut insert or a printed label that must align with a barcode scanner. Write these numbers into your purchase order, and attach photos of the approved sample so there is no room for memory to blur the details.
Finally, test the actual order pipeline with a smaller trial run. Place a modest order first, then inspect it the way your customer would, not just by opening one box from the top. If the trial run arrives with inconsistent stitching, color banding, or mixed hardware finishes, it is far cheaper to pause and correct the process now than to discover the same issue after a container leaves the port.
Why Particle Shape Matters More Than Average Size
Two powders can share the same average particle diameter, yet behave completely differently in a hopper, a mixer, or a coating line. That's because average size flattens the very features that control real-world performance: edges, facets, aspect ratios, and surface roughness. A spherical 50-micron particle and an elongated 50-micron particle do not pack, flow, or sinter the same way, and no single number captures that difference.
Shape governs how particles interlock, slide past one another, and distribute stress under load. Needle-like or plate-like grains tend to bridge across openings, resist compaction, and create anisotropic structures, while rounded particles settle into denser, more predictable beds. In processes like dry powder inhalation or battery slurry mixing, this directly changes dosage uniformity, viscosity, and even electrical contact between active particles.
The mismatch becomes most visible when formulation or manufacturing issues are blamed on 'fine' or 'coarse' fractions, while the actual culprit is a shift in morphology. A modest change in milling conditions can keep the mean size nearly constant but produce more fractured, irregular surfaces that trap moisture or air. So if you're only tracking average diameter, you're watching a shadow while the shape calls the shots.
Sourcing for Extreme Environments: Beyond the Spec Sheet
Real-world sourcing for extreme environments starts with admitting that the spec sheet is only a starting point. A component rated for -40°C might survive a brief cold soak in a lab, but fail after repeated thermal cycling combined with vibration. We've learned to ask suppliers about test conditions that mimic actual use: rapid temperature swings, salt fog after thermal shock, and continuous operation near rated limits. The numbers matter less than the story behind how they were obtained.
Another overlooked factor is material behavior at the interfaces. Seals, connectors, and conformal coatings often degrade before the main component does. A sourcing decision should include a review of mating materials and assembly techniques, not just the part itself. For example, a ruggedized sensor might work perfectly on its own, but when potted in a rigid compound that expands differently at low temperatures, micro-cracks appear around the leads. That's where field failures hide.
Finally, build a shortlist of suppliers who have genuine field data from similar deployments. Ask for failure analysis reports, not just qualification certificates. A vendor who has supported mining equipment in the Atacama Desert or offshore platforms in the North Sea brings tacit knowledge that no datasheet can capture. That experience often translates into practical recommendations like derating guidance, thermal management tweaks, or alternative part suggestions that keep your system alive when conditions turn hostile.
The Real Cost of Cutting Corners on Trace Elements
Skipping trace minerals like zinc, manganese, or copper might trim a few dollars from the upfront budget, but the bill comes due in ways that are easy to overlook. A crop short on zinc doesn't always show dramatic symptoms—just slightly pale leaves, a slower canopy closure, fewer seeds per head. Those small gaps compound across a field, turning what looked like a smart saving into a yield drag that costs far more than the missing nutrient ever would have.
The damage rarely stops at the current season. Trace element depletion in soil builds quietly, year after year, until the buffer is gone. Once boron or molybdenum levels drop below a critical threshold, root development stalls, nitrogen fixation sputters, and even generous applications of NPK can't restore full productivity. Rebuilding that lost fertility can take multiple seasons and a much heavier investment than maintaining adequate levels from the start.
In livestock and poultry operations, the same pattern plays out in slower growth, weaker immune responses, and poor reproductive performance. A feed mix that saves a few cents per ton by reducing selenium or iodine often leads to higher veterinary costs, lower feed conversion, and more animals culled before reaching market weight. The true cost of cutting corners on trace elements isn't measured at the point of purchase—it shows up later in lost output, degraded product quality, and the quiet erosion of long-term productivity.
Negotiating with Vendors Who Understand Your End Use
When a supplier truly grasps how their component or material will be used in your final product, the conversation shifts from price haggling to problem solving. Instead of defending a spec sheet, they start proposing alternatives that could cut costs without hurting performance. This kind of dialogue only works if you share enough detail about your end application early on—otherwise you're both guessing.
A vendor who understands your end use can also flag risks you might have missed. For example, a fabric supplier who knows your garments will be worn in humid climates may suggest a different weave or treatment, even if it costs a bit more upfront. That foresight saves returns, rework, and reputational damage later. In negotiations, this translates into leverage: you're not just buying a part, you're buying their expertise in making your product succeed.
To get there, ask questions that reveal how deeply they've thought about your application. Have them walk through a few failure scenarios or describe how their product behaves under your specific conditions. If they can't engage at that level, the negotiation will stay transactional—and you'll likely leave value on the table. The best agreements come from vendors who are invested in your outcome, not just your purchase order.
FAQ
A dependable vendor shows you the raw data behind every batch—particle size curves, oxygen content, residual boron oxide—without being asked. They also admit when a certain grain size can't hit your tight spec, instead of promising "close enough." Mediocre suppliers tend to hide behind glossy spec sheets and push inventory they already have in stock.
Look beyond the headline "99%" claim. Carbon and oxygen often sneak in and weaken sintered parts. Ask for free boron, boron oxide, and metallic contamination levels separately. A supplier who can tell you the typical oxygen pickup during milling, not just the incoming powder chemistry, understands how their material behaves in your process.
In armor, a bimodal or multimodal distribution packs grains more densely, which improves fracture resistance but can complicate hot pressing. For abrasives, a narrower cut usually gives more predictable material removal. The key is asking for the full D10-D90 curve, not just a median number, because two powders with the same D50 can behave completely differently.
Anyone can ship one perfect sample. Consistency shows up after the fifth or twentieth order, when the powder still behaves the same in your sintering furnace. Ask for SPC charts or historical batch data—if a vendor gets nervous about sharing that, they probably haven't been tracking it.
At minimum, a certificate of analysis showing actual measured values for purity, particle size, and oxygen content—not just pass/fail boxes. For armor-grade material, ballistic test reports tied to specific lot numbers matter more than generic lab certificates. Also request XRD patterns to confirm phase composition, because amorphous boron or free carbon can hide in poorly controlled batches.
If your downstream process—like slip casting, tape casting, or pressureless sintering—needs a very specific particle shape or surface chemistry, generic off-the-shelf powder may force you to adjust your recipe every batch. Paying for a vendor who can tailor surface oxidation or apply a dispersant-compatible coating often saves more in process downtime than the extra material cost.
Ask where the raw boron carbide comes from—bought as powder from a third party or synthesized in-house? Vendors with their own furnaces and milling capacity can usually scale more honestly. Also request lead times for repeat orders of the same spec, not a new prototype. If the answer changes by more than two weeks between quote and purchase, treat that as a warning.
Watch for vague answers about oxygen or carbon content, refusal to share the full particle size distribution, or a certificate of analysis that looks identical across multiple lots. Another tell is when pricing is far below market without a clear explanation—like using lower-grade scrap or skipping proper jet milling classification.
Conclusion
A reliable boron carbide supplier rarely volunteers the full story about their powder. The lot you sample may look impressive on a certificate, but hidden variations in particle size distribution, agglomeration, and surface contamination often only surface after you've committed to a large order. Ask for batch-to-batch consistency data—not just a single data sheet—and request retained samples from previous production runs. Particle shape deserves more attention than the average size number. Irregular, angular grains pack and sinter differently than blocky or rounded ones, changing wear resistance and fracture toughness in ways a simple d50 value cannot capture. If a vendor avoids discussing morphology or only provides a mean diameter, treat that as a warning.
When sourcing for extreme environments—high-temperature armor, neutron shielding, or abrasive blast nozzles—relying on the spec sheet alone is risky. Trace elements like iron, silicon, and free carbon can shift sintering behavior and degrade performance under thermal shock or radiation. A low upfront price often hides less rigorous purification, which becomes painfully expensive when a batch fails in service. The best negotiations happen with vendors who understand your end use and can adjust powder chemistry, surface treatment, or particle size distribution accordingly. Ask them how their material behaves in your specific application, not just whether it meets a generic ASTM or ISO number. A vendor who answers with questions about your process is usually one worth keeping.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/