SiC Coated Graphite Factory Processes That Enhance Semiconductor Manufacturing
2026-10-12
What if the weakest link in your semiconductor line isn't the lithography or etching—but the graphite fixtures inside the chamber? SiC coated graphite has become essential for wafer carriers and susceptors, yet the coating is only as reliable as the factory process behind it. From raw graphite purification to CVD SiC deposition and final inspection, each step either protects your wafers or introduces risk. Semicorex focuses on those process details so fabs don't have to. This post unpacks the factory methods that turn SiC coated graphite into a true manufacturing advantage.
Purifying Graphite to Semiconductor-Grade Levels
Turning run-of-mine graphite into a material suitable for semiconductor applications is less about simple cleaning and more about removing elements that sabotage crystal growth and device yield. Natural flake or vein graphite may look pure, but its ash content often carries iron, aluminum, calcium, silicon, and—most critically—boron. Boron is especially problematic because it acts as an inadvertent dopant in silicon and silicon carbide, shifting resistivity and ruining wafer performance. Reaching semiconductor-grade levels typically means pushing total impurity content below 5 parts per million, with boron often required under 1 part per million.
A practical purification route usually starts with flotation and acid leaching to strip away silicate and oxide minerals, but that alone leaves the graphite far from acceptable. The decisive stage is high-temperature halogen purification: the material is held at 2,500–3,000°C in a chlorine or chlorine-containing atmosphere. At those temperatures, most metal impurities form volatile chlorides and are carried out of the furnace. Vacuum degassing follows to remove residual gases and any remaining low-boiling species. Boron, however, does not form a sufficiently volatile chloride, so producers often add fluorine-bearing compounds or run multiple thermal cycles to bring boron down to specification.
Verification is just as important as the purification itself. Semiconductor-grade graphite is not certified by guesswork—each lot is typically analyzed by glow discharge mass spectrometry or inductively coupled plasma mass spectrometry, with attention to both total ash and the concentration of individual elements like iron, nickel, copper, and boron. Many wafer fabs and crystal growers go further, qualifying a graphite supplier through their own test runs because a single contaminated crucible or susceptor can destroy an entire silicon carbide boule. Only a handful of producers worldwide can reliably deliver graphite at this purity, and even small changes in feedstock or furnace atmosphere can shift the impurity profile enough to fail qualification.
Machining Tolerances That Keep Wafer Carriers Aligned
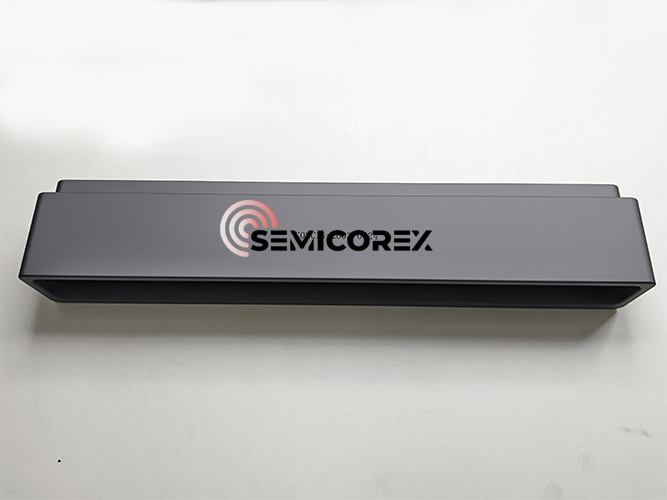
Holding wafer carriers within a few microns of flatness across the entire seating surface is what stops micro-cracks from forming at the edge of a 300 mm wafer. The pockets that receive each wafer are machined with a parallelism tolerance usually under 0.005 mm, so the wafer rests evenly instead of tilting by a fraction of a degree that might go unnoticed until a scanner rejects the lot.
The critical dimensions start with the slot width and pitch. If a carrier slot is machined even 0.02 mm too wide, a wafer can shift during robotic transfer and knock against the slot wall. That kind of contact produces particles, and in a sub-10 nm process those particles become killer defects. A well-controlled machining process will also hold the slot-to-slot pitch within ±0.01 mm, which keeps the handling robot from having to correct its trajectory mid-move.
Beyond the pockets themselves, the base and side rails of the carrier need to be square to the wafer plane. A carrier that is machined with a slight twist can sit unevenly on a load port, forcing the aligner to compensate for a yaw error every time a wafer is extracted. Factories that invest in carriers machined with sub-micron flatness and tight geometric tolerances see far fewer tool-induced shift errors and a measurably lower particle count on monitor wafers.
Growing a Pinhole-Free SiC Layer via CVD
Getting a dense SiC film without pinholes is less about a single magic parameter and more about controlling several failure points at once. In practice, the pinholes that show up in CVD-grown SiC often trace back to particles landing on the wafer, micro-pits left from surface preparation, or droplets formed when the precursor reacts too early in the gas phase. If any of these survive the early nucleation stage, they tend to persist as voids as the film thickens because the growth front simply grows over them rather than filling them in.
One approach that has worked well in pilot runs is to start with an in-situ hydrogen etch at slightly higher temperature before switching to deposition. This removes native oxide and shallow surface damage without aggressively roughing the area around scratches or exposing underlying defects. After that, the first few hundred nanometers are best grown at a lower pressure and with a slight carbon-rich gas ratio; excessive silicon can encourage gas-phase precipitation, and those particles then fall onto the wafer and become pinhole seeds. Keeping the precursor flow modest during the initial stage gives the layer time to merge laterally across atomic steps before vertical growth accelerates.
Temperature uniformity across the susceptor also matters more than it first appears. A cold edge can delay nucleation locally, so the film closes at different rates and leaves a visible seam or small opening where the fronts meet. Some reactors avoid this by using a short buffer layer grown under highly diluted silane, which establishes a smooth SiC surface and then the main layer can grow in a steady step-flow mode. Once that transition is made, the pinhole density typically drops below what optical inspection can easily resolve, especially if the gas flow paths are kept clean and the wafer handling step is kept as short as possible.
Polishing Surfaces to Prevent Particle Shedding
In cleanroom and precision manufacturing environments, even the smallest stray particle can ruin a product or compromise a process. One effective way to reduce this risk is through controlled surface polishing. By carefully smoothing the microscopic peaks and valleys on metal, plastic, or ceramic parts, you eliminate the tiny crevices where dust, fibers, and process residues tend to collect. Over time, these loosely bound contaminants can break free and shed into the surrounding environment, but a polished surface gives them fewer places to hide.
The choice of polishing method matters just as much as the final surface finish. Mechanical buffing and abrasive lapping work well for many metals, but they must be followed by thorough ultrasonic cleaning to remove embedded abrasive grains. For stainless steel components used in semiconductor or pharmaceutical equipment, electropolishing is often preferred because it dissolves a thin outer layer, leaving behind a smoother, more corrosion-resistant surface with far less particle shedding. Even with polymers, a careful vapor polishing or flame treatment can reduce surface roughness and lower the risk of particle release.
It is worth noting that polishing alone is not a one-time fix. Regular inspection under magnification or surface profilometry helps confirm that the finish remains within the required roughness range. In applications where particle shedding must stay extremely low, pairing polished surfaces with a final cleanroom wipe-down using a low-lint solvent can further reduce the chance of contamination. The goal is to create a surface that not only looks smooth but also behaves predictably under real operating conditions, without gradually shedding particles over time.
Firing Cycles That Lock in Thermal Stability
Achieving lasting thermal stability isn't about pushing a kiln to a single peak temperature—it's about choreographing the entire firing curve. A deliberately slow ramp through the quartz inversion zone, for instance, gives crystalline phases enough time to reorganize without trapping micro-stresses. Holding near the maturing point then allows those newly formed bonds to settle, while a stepped cooling phase prevents sudden contraction from undoing the work. This kind of curve locks in dimensional accuracy long before the piece reaches room temperature.
The cooling segment often gets overlooked, but it's where thermal stability is either secured or lost. By controlling the descent through critical temperature windows—especially between 600°C and 400°C for many ceramic bodies—residual stresses are released gradually. The result is a structure that can handle repeated heating and cooling cycles without warping, cracking, or drifting in shape. It's less about the final temperature and more about how time is distributed across the entire thermal journey.
Cleanroom Inspection Before Shipping to Fabs
Prior to any shipment leaving our facility, every component undergoes a rigorous cleanroom inspection tailored to the exacting standards of semiconductor fabs. This is not a cursory glance—each item is examined under controlled airflow and particulate monitoring, with special attention to surface cleanliness, edge integrity, and absence of micro-contamination that could compromise wafer yield. Our inspectors use bright white LED arrays and oblique lighting to reveal even sub-micron residues that standard room lighting would miss.
Beyond visual checks, we perform tape lift tests on representative surfaces and immediate particle counting via laser-based airborne and surface scanners. Any unit exceeding Class 1 cleanroom particle limits is quarantined and re-cleaned using a two-stage ultrasonic process with ultrapure water and IPA drying, then re-inspected from scratch. Packaging is only permitted inside the cleanroom itself, using static-dissipative film and vacuum-sealed double bags, with a final label logged against the fab's own incoming inspection criteria.
What sets this step apart is the human element: inspectors rotate between fabs' specific checklists, learning the subtle differences between a TSMC-approved surface finish and a Samsung-grade edge polish. That accumulated memory means less false rejects, fewer surprises at the fab's own metrology bay, and a shipment that arrives ready for tool install—not another round of cleaning on the dock.
FAQ
Silicon carbide coating on graphite combines the substrate's machinability with a surface that resists oxidation, chemical attack, and particle shedding. In wafer processing, this means fewer contaminants and longer-lasting fixtures for epitaxy, ion implantation, and plasma etch chambers.
Most facilities use chemical vapor deposition (CVD) at high temperature, flowing methyltrichlorosilane and hydrogen over graphite parts inside a vacuum reactor. The process builds a dense, pinhole-free silicon carbide layer that conforms to complex shapes, including holes and threaded features.
Before deposition, the graphite is machined, ultrasonically cleaned, and often subjected to a high-temperature vacuum bake to remove moisture and organic residues. A controlled surface roughening step can also be used to create mechanical interlocking, while gradual thermal ramping during CVD prevents delamination from thermal expansion mismatch.
Graphite naturally contains metallic impurities that can diffuse into the SiC layer during high-temperature processing. Factories use halogen gas purification at temperatures above 2000°C to drive out these metals, ensuring the final coated part does not release harmful elements into sensitive semiconductor processes.
The SiC coating acts as a protective barrier, but the underlying graphite must have appropriate grain structure and density. By selecting fine-grain, high-density graphite and applying a uniform coating with controlled thickness, factories produce susceptors and wafer carriers that withstand rapid heating and cooling cycles without cracking or spalling.
Coated parts are inspected using eddy current testing or X-ray fluorescence to map coating thickness, while scanning electron microscopy checks for pinholes or microcracks. Factories also perform thermal cycling tests and particle count analysis to ensure the coating remains intact under simulated wafer processing conditions.
Yes, process parameters such as coating thickness, surface roughness, and final polishing can be adjusted to match the requirements of different tools like MOCVD reactors, rapid thermal processing chambers, or etch electrodes. Some factories also offer selective coating or masking to keep certain graphite areas exposed for electrical contact or clamping.
Conclusion
At the heart of every high-yield semiconductor fab lies a quiet obsession with contamination control, and SiC coated graphite factories have turned that obsession into a multi-step ritual. It begins not with coating, but with raw graphite purification, where trace metals like iron and copper are driven down to parts-per-billion levels using high-temperature halogen gas treatments. Only then can machining tolerances of ±5 microns be trusted—because a wafer carrier that shifts by a fraction of a millimeter during epitaxy creates thermal gradients that ruin entire batches. The real differentiator, though, is the CVD-grown silicon carbide layer. Instead of a porous, uneven spray coating, a dense, pinhole-free film is deposited atom by atom, sealing the graphite against reactive process gases like hydrogen and ammonia. This layer is then polished to a mirror finish, not for aesthetics, but to eliminate micro-roughness where particles would otherwise shed onto wafers.
Thermal stability doesn't come from the SiC alone—it comes from firing cycles that subject each carrier to repeated ramps above 1600°C in inert atmospheres, forcing the graphite substrate and coating to reach dimensional equilibrium before they ever enter a customer's furnace. Without this step, a carrier could warp on first use, causing wafer slip and costly downtime. Finally, nothing leaves the factory without cleanroom inspection under particle counters and bright-field lights, where a single embedded particle or edge chip means the part is scrapped. These processes may sound like overkill, but in semiconductor manufacturing, the difference between a 60% yield and a 90% yield is often traced back to something as mundane as a graphite carrier that didn't shed, didn't warp, and didn't react. That is what a well-run SiC coated graphite factory delivers—not just a component, but a predictable foundation for advanced chip production.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com