Top 10 Corrugated Pipe Machines for Reliable Pipe Production
2026-10-21
If you're sourcing equipment for corrugated pipe production, the word reliable gets thrown around a lot — but what actually separates machines that run shift after shift from the ones that stall after a few months? This list of top 10 corrugated pipe machines digs beyond spec sheets and glossy brochures, focusing on real-world uptime, maintenance headaches, and the small design choices that make a big difference. Among the names worth watching is COMRISE, a manufacturer that has quietly built a reputation for machines that hold tolerance when line speed climbs. Whether you're upgrading an existing line or planning a new facility, the following breakdown gives you a practical starting point — no fluff, just the details that matter when downtime is measured in dollars.
What actually separates a corrugated pipe machine that holds tolerance from one that drifts after a month
The difference often comes down to how the machine frame and base castings are stress-relieved and machined. A machine that holds tolerance typically uses a heavier, normalized steel or cast iron frame with mating surfaces ground after welding, so thermal expansion and vibration don't slowly shift alignment. Cheaper machines skip this step; residual stresses from fabrication relax over the first few weeks of production, causing the extruder centerline to move by a few thousandths, which shows up as wall thickness variation or diameter drift.
Another separator is the quality of the screw and barrel plus the control loop tuning. Machines that stay stable use nitrided or bimetallic barrels and screws with hard-facing on the flights, paired with temperature controllers that actually hold setpoint within a degree or two. When the barrel has soft spots or the PID parameters are left at factory defaults, the material viscosity swings with ambient temperature and regrind percentage, and the pipe wall slowly creeps out of spec. You see it after about a month because that's how long it takes for screw wear to start showing in backpressure.
There's also the downstream calibration and haul-off. A machine that holds tolerance has vacuum calibration sleeves that are independently adjustable and a haul-off with a load cell or torque feedback so the pulling force stays constant. If the calibration sleeve is clamped rigidly and the haul-off has a simple open-loop drive, any change in friction, melt temperature, or cooling water temperature translates directly into ovality or longitudinal thickness variation. The drift doesn't happen overnight; it accumulates as the cooling system picks up scale or the vacuum pump filters clog, and after a month the pipe is no longer round enough.
The material handling tricks that stop jams before they eat your shift
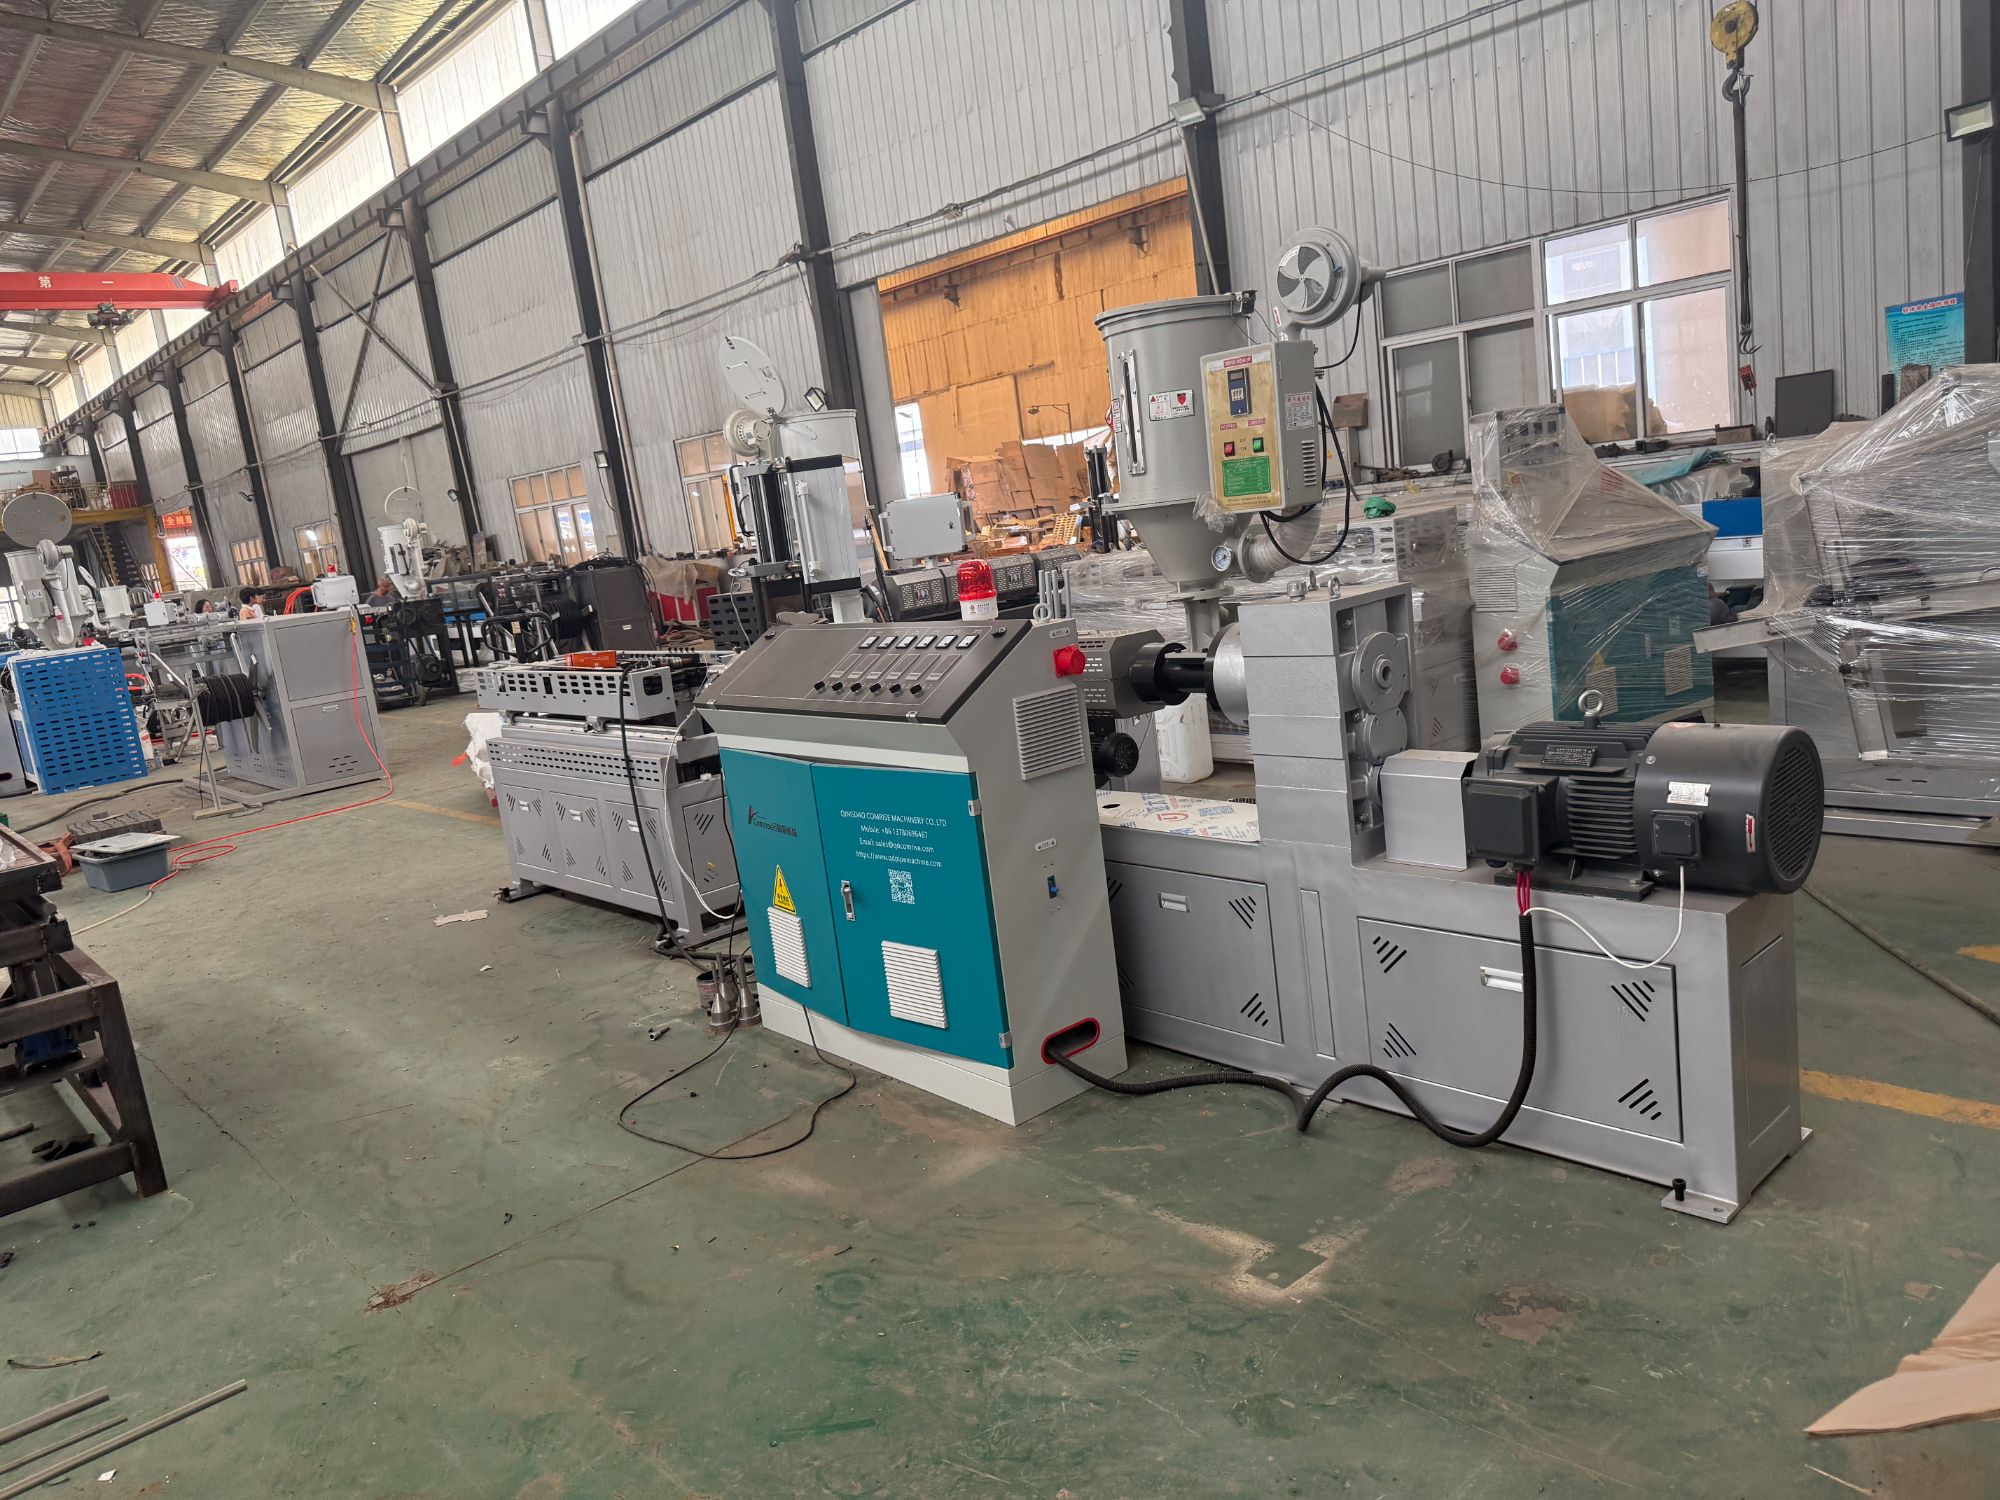
Jams rarely start with a bang. They begin with a cardboard flap folded the wrong way, a belt tracking a few millimeters off, or a sensor lens that caught a film of dust during the last shift. The operators who keep lines moving don't wait for the screech of a stalled roller — they walk the first ten feet of every infeed with their eyes on the angle of each box. A slight skew at the merge point gets fixed with a twist of a guide rail, not a maintenance ticket. That habit of micro-adjusting before the jam forms is what separates a smooth run from a half-hour wrestling match with crushed packaging.
Another trick is learning the sound of your line when it's healthy. A conveyor that hums at a steady pitch, a sorter that clicks without hesitation — these are baselines. When the pitch drops or a new rattle appears near the divert shoe, it's a warning. Skilled handlers will tap the side of a chute, listen for the dull thud of a hidden wedge, and clear it with a short blast of air before it becomes a wall. They also rotate their most problematic SKUs earlier in the shift, when patience and attention are sharp, rather than letting a known offender hit the line at hour seven.
Finally, the best jam prevention is boring: pre-shift walkarounds that actually touch the hardware. Run a hand along each side rail to feel for burrs or sticky residue. Check the photo eyes with a piece of scrap cardboard, not just a visual glance. Loosen and retighten the same two bolts on the transition plates every Monday. None of this shows up on a dashboard, but it builds a kind of muscle memory in the line itself. When the system knows what "normal" feels like, the first sign of trouble shows up as a tiny variation — not a total stop.
Why cooling zone design matters more than maximum speed ratings
The obsession with top speed ratings on cooling fans overlooks a far more practical concern: how air actually moves through the zone you are trying to cool. A fan screaming at 3000 RPM might push impressive cubic feet per minute in open air, but drop it behind a restrictive mesh filter or wedge it against a heatsink with tight fin spacing, and that number collapses. The cooling zone design — the geometry of intake gaps, the path air takes across hot components, and the distance between the fan and the surface it is cooling — determines whether that airflow does useful work or just churns uselessly in a dead pocket.
Think of a laptop hinge area or a PCIe card sandwiched between two others. The maximum speed rating tells you nothing about how well air curls around the corner into a 6mm gap, or whether a dead spot forms right over the voltage regulator. A well-designed cooling zone with a modest 1200 RPM fan can outperform a poorly laid out zone with a 2500 RPM fan simply because the slower fan's air is guided across the right surfaces instead of bouncing off a flat wall. Turbulence, backpressure, and vent placement matter more than raw blade velocity once you move beyond open test benches.
That is why a hand-sized heatsink with carefully angled fins and a small dedicated duct routinely beats a larger heatsink bolted to a faster fan in poorly thought-out enclosures. Speed ratings are easy to print on a box. Zone design requires thermal imaging, smoke tests, and trial and error — the unglamorous work that separates a cooling solution that quietly keeps components at 65°C from one that spins loudly and still throttles under load.
Mold block alignment checks that cut scrap and extend tooling life
Alignment checks on mold blocks often get rushed or skipped until problems show up, but the cost of that neglect shows quickly in flash, uneven wall thickness, and burned material. A simple indicator sweep across the parting line before every run catches offsets as small as a few thousandths that would otherwise force a shutdown and scrap the first dozen shots.
The real payoff comes from tracking how those readings drift over time. Write down the numbers from each setup—dial positions at the corners and center, gap feeler results under no clamp load, and any shim adjustments made. Within a month you'll see patterns that point to worn leader pins, plate warpage from overheating, or a press platen that isn't square. Fixing those root causes keeps the block seated flat, which means vents stay open, flash disappears, and the tool doesn't hammer itself apart on every cycle.
If you can turn alignment checks into a ten-minute routine with a magnetic base and a test indicator, the scrap rate drops without chasing process settings. And because the mold isn't fighting itself, the parting line stays sharp longer, ejector pins stop bending, and the tool can run additional years before a rebuild.
Realistic throughput figures for different pipe diameters and wall thicknesses
Throughput isn't just a function of pipe diameter—wall thickness quietly reshapes the internal cross-section in ways that standard charts often miss. A 100 mm pipe with a 10 mm wall carries noticeably less fluid than the same nominal size with a 5 mm wall, yet most quick-reference tables gloss over that gap. For instance, moving from Schedule 40 to Schedule 80 on a 50 mm line can drop effective flow area by roughly 20%, which translates to lower velocities at the same pump setting or a need for higher pressure to hit the same volume.
Field measurements tell a more useful story. A 25 mm tube with a 2 mm wall might push 40 liters per minute under 3 bar, but bump the wall to 4 mm—same outer diameter—and that figure falls to around 33 liters per minute at identical pressure. The difference comes down to friction losses along the rougher, narrower bore and the extra turbulence near the inner surface. Operators who ignore this often end up oversizing pumps or underestimating fill times, especially in viscous or slurry service where wall roughness amplifies the penalty.
Practical throughput also dips with longer runs and tighter bends, but wall thickness sets the baseline. For gravity-fed systems, a 150 mm pipe with 6 mm walls can drain a 10,000-liter tank in under eight minutes, while the same diameter with 12 mm walls stretches that to nearly eleven minutes. Rather than trusting catalog maxima, a quick calc using actual inside diameter and measured pressure drop gives numbers you can rely on when scheduling batches or sizing filters downstream.
The maintenance mistakes that quietly shorten machine life in busy plants
In busy plants, the most damaging maintenance mistakes rarely come with alarms or breakdowns. They show up as that slow drip from a hydraulic fitting everyone has learned to ignore, or the air filter that gets tapped out instead of replaced. Each small shortcut seems harmless on its own, but together they force motors to run hotter, pumps to work harder, and bearings to carry more debris than they were designed for. Over time, this constant background stress cuts thousands of hours from equipment life without ever showing up on a failure report.
Lubrication is another area where good intentions go wrong. Adding grease until it purges from the seal might feel thorough, but over-greasing actually raises housing pressure, breaks down seals, and pushes contaminants into the rolling elements. Even more common is mixing different grease thickeners because the right cartridge isn't on hand. The resulting incompatibility can turn lubricant into a stiff, waxy paste that offers almost no film protection, leaving gears and bearings to wear metal-on-metal while the maintenance log still shows "lubricated" on schedule.
What makes these failures especially frustrating is that they are almost never corrected because the plant is too busy to stop. Vibration data gets collected but not reviewed until after a failure. Oil samples sit on a shelf waiting for a lab report that nobody reads. The machine keeps running, and the plant hits its production targets right up until the moment a minor issue becomes a major rebuild. Shifting the mindset from "run it until it breaks" to "protect the next shift" is often the single biggest improvement a maintenance team can make.
FAQ
Focus on the pipe diameter range, material compatibility, and how easily you can swap molds. A machine that handles multiple polymers without constant recalibration will save you more downtime than a lower upfront cost.
Most modern models come with intuitive touchscreen controls and preset recipes, but you'll still want at least one technician who understands extrusion temperatures and cooling rates. The learning curve is shorter than older hydraulic systems.
Daily checks on the corrugator blocks and screw wear every 500 hours are a good baseline. Ignoring the small stuff, like bearing lubrication, leads to sudden failures that no top 10 list can prevent.
Some higher-end models offer interchangeable forming tunnels, but it's not universal. Check whether the corrugator can run at different vacuum levels; that flexibility is more important than the machine's position on a list.
Proper cooling controls the pipe's ovality and wall thickness consistency. Machines with multi-zone water spray systems tend to outperform those with simple immersion tanks, especially at production speeds above 15 meters per minute.
Yes, tooling changes, energy consumption, and spare corrugator blocks add up quickly. A slightly more expensive machine with energy-efficient motors and locally available parts often costs less over five years than a cheaper import.
Ask for actual runtime data from existing users, not just the manufacturer's claimed MTBF. Visit a plant running the same model for over 8,000 hours and watch how they handle block changes and emergency stops.
PLC-based systems are usually easier to service and upgrade, but a well-designed dedicated controller can offer faster parameter changes. For most shops, a PLC from a major brand like Siemens or Allen-Bradley reduces troubleshooting time.
Conclusion
A reliable corrugated pipe machine rarely earns its reputation from a spec sheet. The models that hold tolerance month after month tend to share a few overlooked traits: frame rigidity, consistent mold block guiding, and cooling channels that pull heat away evenly instead of just chasing a fast cycle. In busy plants, the difference between a machine that drifts and one that stays steady often comes down to how material feeds, not just how fast it extrudes. Small changes in hopper angle, screw temperature zones, or vacuum calibration can stop jams before they interrupt a shift, which matters more than peak output on day one.
Top ten lists often fixate on maximum speed ratings, yet real throughput depends on pipe diameter, wall thickness, and how well the cooling zone matches the polymer flow. Mold block alignment checks, done weekly rather than after visible scrap appears, extend tooling life and trim waste. Plants that skip these checks or ignore minor wear in drive chains quietly shorten machine life, even when the extruder still appears to run fine. The best choices for dependable production combine robust cooling, accessible maintenance points, and honest throughput figures for the sizes you actually run, not just the headline number that looks impressive on a brochure.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com