Top 10 MOCVD Susceptors for Reliable High-Volume Semiconductor Manufacturing
2026-10-06
In high-volume semiconductor manufacturing, your MOCVD susceptor is more than a consumable—it’s a yield driver. But with a flood of options claiming reliability, how do you build a shortlist that actually holds up under thermal cycling and aggressive process chemistries? This ranking of the top 10 MOCVD susceptors cuts through vendor noise, featuring field-proven designs from Semicorex and other key suppliers to help you make a confident, production-ready choice.
What Really Separates a Production-Grade Susceptor From a Lab Prototype
A lab prototype susceptor usually works under ideal conditions: stable power input, controlled ambient temperature, and a single-use cycle. Production-grade versions, however, face thermal cycling, mechanical vibration, and exposure to process gases or cleaning agents. The real difference isn't the base material—it's how the part holds up when the oven door opens mid-run, or when a power spike hits. Most lab prototypes fail quietly: warping at 400°C, delaminating after fifty cycles, or losing surface emissivity because the coating wasn't matched to the substrate's expansion rate.
Production-grade susceptors earn their name through repeatability, not just initial performance. A lab part might reach target temperature in eight seconds on day one; a production part does it on day four hundred, after being dropped once during maintenance and wiped with a solvent that would etch a lab coating. The distinction often comes down to edge termination, bond line thickness, and whether the supplier has a documented lot-to-lot thermal profile. If you can't get the same heat-up curve from two different batches, you don't have a production part—you have a lucky prototype.
Then there's the matter of failure modes. Lab prototypes tend to crack spectacularly or short out when pushed. Production-grade susceptors are engineered to degrade predictably: a gradual resistance drift that triggers replacement before catastrophic failure, or a surface that oxidizes without flaking conductive particles into the process chamber. Ask a lab supplier about mean time between failures and you'll get a shrug; ask a production supplier and you should get a spec sheet with operational life under different duty cycles. That paper trail, more than any material choice, is what separates the two.
Coating Choices That Survive Thermal Cycling Without Cracking
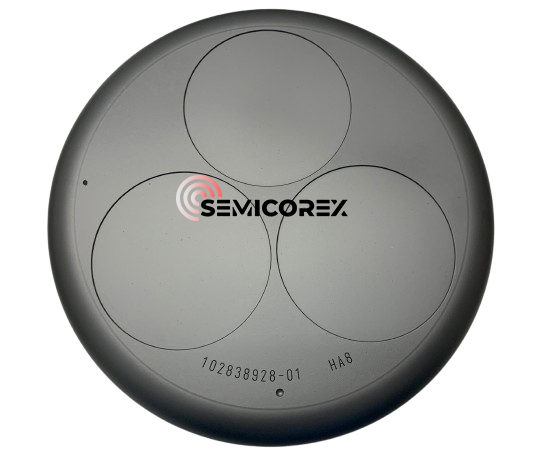
When a coated component endures repeated temperature swings, the mismatch in thermal expansion between the substrate and the coating often turns into the primary failure driver. Instead of chasing the highest hardness or the slickest finish, focus on materials that flex with the base metal rather than fight it. Nickel-chromium-aluminum-yttrium (NiCrAlY) formulations, for example, bring a ductile metallic binder that absorbs strain at grain boundaries, while embedded ceramic particles provide wear resistance without forming a brittle, continuous network. Another practical route is to apply a thin bond coat engineered to have a coefficient of thermal expansion that sits between the substrate and the topcoat, effectively acting as a stress-relief layer during rapid heating and cooling cycles.
Real-world survival also hinges on deposition quality and post-processing. A dense, fine-grained microstructure with low residual stress—achieved through controlled thermal spray parameters or optimized physical vapor deposition—holds up far better than a porous or over-stressed layer that invites crack initiation at micro-defects. Shot peening or laser shock peening after coating can further drive compressive residual stress into the surface, counteracting the tensile stresses that thermal cycling imposes. Finally, don't overlook the role of coating thickness: a thinner, well-adhered layer often outperforms a thick one under cyclic thermal loading, since the strain energy stored per unit area drops and interfacial shear stresses stay manageable. Choosing a coating that prioritizes strain tolerance over absolute hardness is the difference between a surface that outlasts the part and one that flakes off after a few hundred cycles.
Thermal Uniformity Metrics That Predict Wafer-Level Yield
Most fabs still lean on average wafer temperature as a go/no-go signal, but that number hides the real story. A 2°C mean shift might be harmless, while an 8°C edge-to-center gradient during anneal can push local CD or sheet resistance outside the allowed window.
Three spatial metrics deserve attention: within-wafer temperature range, radial gradient (center-to-edge slope), and hotspot density above a threshold. The range captures worst-case spread; the radial gradient flags systematic non-uniformity from lamp arrays or chuck design; hotspot density detects transient local excursions that often correlate with defect nucleation. In production data, these metrics show tighter correlation to die yield than simple mean or max temperature because they reflect the spatial distribution of process rate variations across the wafer.
Rather than relying on single-threshold alarms, teams build logistic regression or random forest models that map these thermal metrics to wafer map yield. Inputs typically include pre- and post-process thermal snapshots, the temperature ramp rate, and the location of any excursion relative to die layout. Once fitted on historical lots, the model can flag at-risk wafers before electrical test, allowing rework or disposition. The key is to keep the metric set small enough to avoid overfitting while ensuring it captures both global and local non-uniformity.
Why Pocket Geometry Matters More Than You Think in High-Volume Runs
In high-volume machining, pocket geometry is not a cosmetic detail. Corner radii, wall draft angles, and floor-to-wall transitions directly control how cutting forces build and release. A sharp 90-degree internal corner forces the tool to make an abrupt direction change, spiking radial load and inviting chatter. Add even a modest radius and that same corner spreads engagement across a longer arc, letting you hold higher feed rates without destroying end mills.
Chip evacuation and coolant access depend on geometry too. Deep pockets with perfectly vertical walls trap chips against the cutter, causing recutting, heat buildup, and unpredictable tool wear. A slight taper or a larger corner radius gives chips a natural escape path while allowing coolant to reach the cutting zone. This becomes critical when you are running thousands of parts unattended; a single chip jam can scrap a batch before anyone notices.
What catches most shops off guard is process drift. If pocket geometry invites vibration or uneven tool engagement, you will constantly tweak offsets, swap tools mid-shift, and lose cycle time to rework. Geometries that distribute load and clear chips smoothly keep the process stable across an entire run. In that context, pocket design stops being a minor engineering choice and becomes the difference between a reliable production cell and a machine that needs constant babysitting.
Maintenance Patterns That Extend Susceptor Life Beyond Standard Specs
Most susceptor failures trace back to thermal cycling habits rather than raw operating hours. Ramping at moderate rates, holding at intermediate plateaus before full power, and letting the part cool under controlled atmosphere reduce micro-crack initiation in the SiC coating. In practice, shops that replace aggressive ramp profiles with a stepped bake-out schedule often see coating adhesion remain intact well past the manufacturer’s stated cycle count.
Cleaning frequency matters less than how residues are removed. Dry ice blasting or gentle chemical wipe-downs with approved solvents prevent carbon buildup without eroding the coating edges. After each cleaning, a low-temperature inert bake removes absorbed moisture and volatile leftovers, which otherwise turn into localized hot spots during deposition. Rotating the susceptor on its support and re-torquing fasteners in a star pattern keep contact stress evenly distributed.
Storage and inspection routines complete the picture. Keeping susceptors in nitrogen-purged cabinets, resting them on soft graphite felt instead of metal racks, and documenting surface roughness changes help catch early pitting or edge chipping. A short pre-run plasma clean or hydrogen bake can restore surface condition before it degrades to the point of replacement.
Material Purity Trade-Offs When Scaling From Pilot Lines to Full Production
Pilot lines tend to operate with tightly controlled, often premium-grade precursors because small batch sizes can absorb the cost of high purity without wrecking the economics. Once a process moves to full production, purchasing shifts to bulk suppliers and larger lot sizes, which can introduce subtle variations in trace metals, moisture content, or organic residues that were never visible at the pilot scale. These impurities rarely cause immediate failures, but they can shift doping levels, alter grain boundary behavior, or reduce long-term stability in ways that only show up after hundreds of cycles or hours of operation.
The real trade-off is seldom about whether purity should be maintained, but about which impurities matter and how much tolerance can be built into the downstream steps. Full-scale purification methods such as additional recrystallization, longer distillation columns, or more aggressive washing add both capital and operating expense, yet they may deliver diminishing returns if the final device performance is insensitive to a particular contaminant. Engineers often find themselves re-validating the entire process because a formerly negligible impurity becomes significant when mixing tanks, transfer lines, and drying ovens operate under different thermal and mechanical stresses than the pilot setup.
A practical way to manage this transition is to stop treating purity as a single number and instead monitor a handful of known problematic species using inline analytics or rapid sampling. By correlating impurity levels with yield and reliability data from the first production runs, it becomes possible to set realistic specifications that avoid both the over-engineering of needless purification and the risk of field failures from overlooked contaminants. This shift from absolute purity to impurity profiling is often what separates a smooth scale-up from one that quietly accumulates rework and warranty costs.
FAQ
In high-volume manufacturing, the difference shows up after hundreds of thermal cycles. A production susceptor holds pocket depth, flatness, and coating adhesion far longer, so wafer-to-wafer temperature profiles stay consistent. Lab-grade parts often work fine for a few runs but start drifting once they face ammonia, hydrogen, thermal shock, and robotic handling every day.
SiC-coated graphite still dominates because it pairs chemical inertness with good thermal conductivity and a reasonable price. Molybdenum and tungsten appear in some low-pressure or high-temperature steps, but they're heavier and trickier to machine into complex pockets. Tantalum carbide coatings are gaining ground where longer campaigns and reduced particle shedding matter more than upfront cost.
Enough that experienced process engineers treat pocket depth, sidewall angle, and rim flatness as first-order variables. A pocket that's too deep traps gas and shifts the thermal boundary layer; one that's too shallow lets the wafer move or bow. Small differences across a batch can create edge slip, non-uniform doping, or thickness variation that only shows up at final test.
Avoid thermal shock by controlling ramp rates after maintenance. Use dry ice or CO2 snow for routine residue removal instead of aggressive scraping. Keep the susceptor in a clean, dry box when it's not in the reactor, and never touch the coated surface with bare hands. If you see a microcrack or a dull patch, pull it before it becomes a particle source.
No. The real math includes how many runs you get before recoating, how much yield drops as the coating ages, how long the reactor sits idle during swaps, and whether a failing susceptor can damage wafers or downstream parts. A cheaper part that needs replacement twice as often and scrapes a few wafers can easily cost more than a premium one.
Some can, but only after you qualify them like any other critical consumable. Check coating thickness, impurity levels, pocket tolerances against your reactor spec, and whether the vendor has data from the same process chemistry. It's also worth confirming whether your equipment supplier will still support the chamber if a third-party part is installed, because that can quietly void a service contract.
It depends on what you're optimizing. A heavier susceptor smooths out temperature swings during wafer transfer and can improve repeatability, but it slows ramp rates and recovery after maintenance. A lighter design responds faster and can shorten cycle time, yet it may amplify small heater fluctuations. The best choice balances throughput against the uniformity your epi layers actually demand.
Typically three to five cycles if the graphite core is still sound. Each recoating removes a little base material, so pocket dimensions and flatness need to be re-verified. Once you see oxidation in the graphite, warping beyond spec, or repeated coating delamination, further recoating becomes a false economy.
Conclusion
Selecting a reliable MOCVD susceptor for high-volume semiconductor manufacturing demands attention to factors that go far beyond laboratory curiosity. A production-grade unit must survive repeated thermal cycling without the coating delaminating or micro-cracking, which is why manufacturers increasingly favor SiC or engineered graphite with tailored CVD layers over cheaper prototypes. Thermal uniformity, measured across the full wafer pocket at operating temperature, directly predicts yield, and top-tier susceptors maintain a tighter delta than the human eye can appreciate. Pocket geometry also plays a quiet but decisive role: subtle changes in sidewall angle and depth affect gas flow and film thickness, leading to yield variations that only become visible when runs scale into the thousands.
Material purity trade-offs become sharper when moving from pilot lines to full production, as trace impurities that were tolerable in short runs start to degrade device performance over longer campaigns. Maintenance patterns, including clean cycles and conditioning steps, can extend susceptor life well beyond standard specifications, but only if the coating remains intact and the graphite substrate stays dimensionally stable. The best high-volume susceptors combine a predictable wear rate with easy refurbishment, allowing fabs to plan replacements without surprise downtime. In practice, the top ten options share a common trait: they balance thermal stability, mechanical robustness, and cost per wafer pass in a way that makes sense outside the lab.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com